
— Blogs —
—Products—
 Consumer hotline +8618073152920
WhatsApp:+8615367865107
Address:Room 102, District D, Houhu Industrial Park, Yuelu District, Changsha City, Hunan Province, China
Product knowledge
Time:2026-08-27 09:02:00 Popularity:172
Selecting Ec Sensor Turbidity Sensor starts with the suspended-solids range, optical path, installation geometry and cleaning access at the actual water point. The engineering test for Ec Sensor Turbidity Sensor is its ability to withstand the installation environment, exchange data with the controller and maintain readings that remain credible after handover.
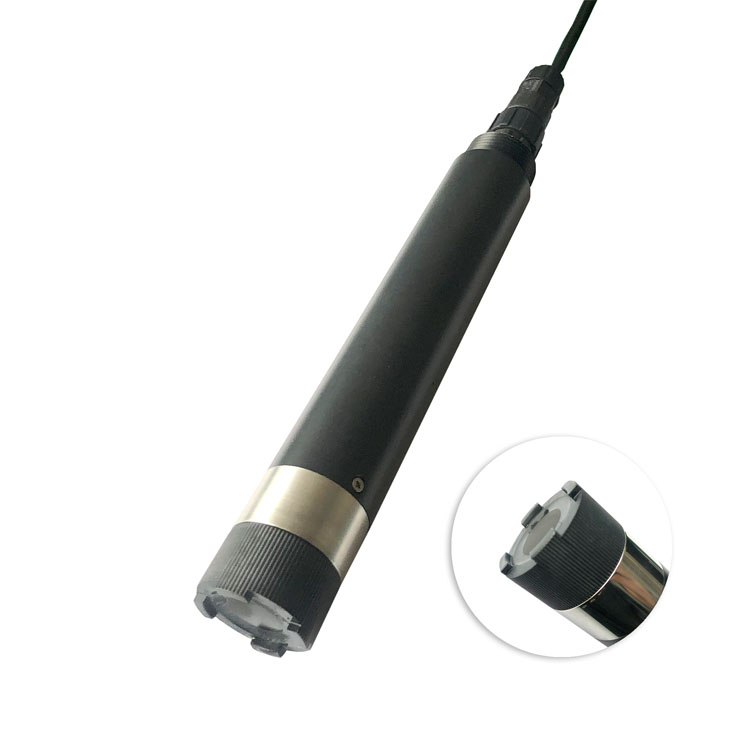
An EC and turbidity monitoring point combines two measurements that respond to different water conditions. Conductivity indicates changes in dissolved ionic content, while turbidity responds to suspended material and optical interference. The project specification should therefore define the purpose, expected range, installation arrangement and maintenance method for each channel separately.
For ec sensor turbidity sensor, the buyer should write the use case in one sentence before comparing suppliers. For ec sensor turbidity sensor, the use case should identify whether the measurement supports process control, an alarm, an operating schedule, a reference record or an environmental warning. Defining that duty for Ec Sensor Turbidity Sensor determines the range, interface, accessories and evidence required at handover.
The short answer: choose ec sensor turbidity sensor by application, output and installation method. Do not buy by product term alone. A complete Ec Sensor Turbidity Sensor package must align the field device, cable, mounting hardware, power, controller interface and acceptance procedure.
For ec sensor turbidity sensor, maintenance cost and spare probe planning should be written into the purchase file. For Ec Sensor Turbidity Sensor, a comparable quotation should separate the sensing assembly, signal interface, cable, mounting accessories and commissioning services required by the stated site conditions.
If the project includes several monitoring points, create a small point list for ec sensor turbidity sensor: ID, location, cable length, Modbus address, parameter unit and maintenance note. The Ec Sensor Turbidity Sensor point schedule becomes the common reference for address assignment, commissioning records, maintenance history and later system expansion.
For ec sensor turbidity sensor, remote station power and telemetry reliability should be written into the purchase file. For Ec Sensor Turbidity Sensor, a comparable quotation should separate the sensing assembly, signal interface, cable, mounting accessories and commissioning services required by the stated site conditions.
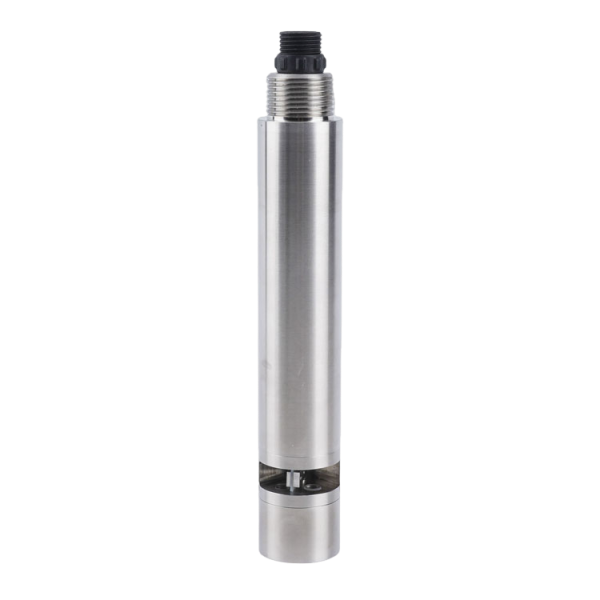
For ec sensor turbidity sensor, Modbus communication should be checked against the actual water quality cabinet: register address, unit, decimal place, temperature compensation value and alarm polling interval all need to be confirmed before shipment.
For ec sensor turbidity sensor, the cable route should be checked against pumps, dosing lines and aeration equipment. The turbidity sensor cable route, shield termination, grounding arrangement and junction-box location should be verified with the control-panel design before installation.
| Parameter | Typical project value | Procurement meaning |
|---|---|---|
| Measurement range for turbidity sensor | Selected by parameter and water matrix | Prevents low resolution or overload at the alarm point |
| Accuracy for turbidity sensor | Project-grade online accuracy after calibration | Supports trend alarms and process control |
| Power supply for turbidity sensor | DC 12-24 V | Fits water quality cabinets and solar monitoring points |
| Output for turbidity sensor | RS485 Modbus RTU | Allows direct connection to PLC, RTU, data logger or IoT gateway |
| Protection for turbidity sensor | IP68 probe or flow-through assembly | Matches immersion, tank, channel or pipeline installation |
| Maintenance for turbidity sensor | Cleaning and calibration interval by fouling level | Often decides long-term data reliability |
For Turbidity sensor, parameters matter only when they are tied to field decisions. For Turbidity sensor, range protects measurement headroom, accuracy supports the required decision, output defines controller compatibility and wetted materials determine service life in the medium.
In aquaculture, conductivity trends can reveal changes in salinity or dissolved content, while turbidity may rise after feeding, pond disturbance or solids accumulation. The logger interval and alarm logic should preserve these short events and distinguish a process change from fouling, bubbles or a disturbed optical face.
Integration plan for Turbidity sensor: Install online sensors with RS485 output and safe retrieval for cleaning.
Project value: continuous Turbidity sensor data provides earlier warning of unstable water conditions and gives operators a record for evaluating corrective action.
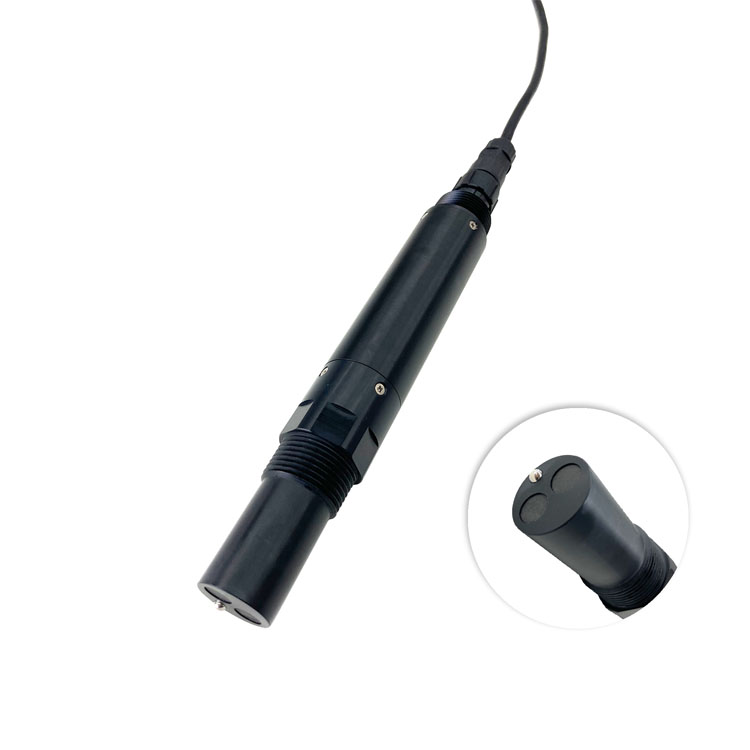
At a wastewater point, position the turbidity optical path away from persistent bubbles and settled sludge while keeping it exposed to representative flow. Place the EC electrodes where deposits can be inspected and cleaned. Cleaning frequency should be set from observed drift and fouling, not copied from an unrelated site.
Integration plan for Turbidity sensor: select a serviceable probe position, provide secure mounting and leave enough access for inspection, cleaning and reference checks without interrupting the process unnecessarily.
Project value: online Turbidity sensor trends show changes between laboratory sampling rounds and support a faster, documented operating response.
Field challenge: At a river or source-water site, Turbidity sensor must remain representative as water level, debris load and biological growth change through the season.
Map the EC and turbidity channels independently in the controller, including address, register, data type, decimal scale, unit and invalid-value handling. Protect the probe and cable without creating a stagnant pocket, and retain timestamped local data whenever the uplink is unavailable.
Project value: reliable Turbidity sensor trends help operators distinguish a developing water-quality change from a short communication or maintenance event.
For turbidity sensor, the specification should name the operating decision first. Where Turbidity sensor data initiates an alarm, the specification should identify the threshold, delay logic, responsible operator and required response rather than relying on a feature list. Where Turbidity sensor supports reporting rather than control, stable sampling intervals, timestamps, engineering units and export format become the principal data requirements.
A supplier comparison for turbidity sensor should separate the sensor, accessories, controller interface, mounting hardware, documentation and after-sales support. Separating these scope items allows Turbidity sensor offers to be compared on equivalent hardware, integration and service responsibilities.
The practical acceptance test for turbidity sensor is not only powering on the device. Handover for Turbidity sensor should demonstrate a valid live reading, successful controller communication, the intended alarm path and one routine service procedure performed by site staff.
For long-term operation, turbidity sensor should be purchased with a spare-parts view. For Turbidity sensor, cable assemblies, mounting parts and service consumables should be reviewed as availability-critical items because a missing minor component can stop a monitoring point.
Before requesting a quotation for turbidity sensor, provide the application site, expected measuring range, installation method, power supply, required output, cable length, quantity, destination country, accessories and whether local display or remote platform upload is required.
For turbidity sensor, controller integration and Modbus register mapping should be written into the purchase file. For Turbidity sensor, a comparable quotation should separate the sensing assembly, signal interface, cable, mounting accessories and commissioning services required by the stated site conditions.
For Turbidity sensor, use one pilot point before bulk delivery when the site condition is uncertain. Before releasing a volume order For turbidity sensor, the pilot point should confirm mounting, signal stability, cable routing, service access and end-to-end data delivery under site conditions.
For turbidity sensor, sample representativeness and installation point should be written into the purchase file. For Turbidity sensor, a comparable quotation should separate the sensing assembly, signal interface, cable, mounting accessories and commissioning services required by the stated site conditions.
The project should evaluate turbidity sensor mainly from the angle of sample representativeness and installation point. For Turbidity sensor, that operating focus changes the required evidence for sample representativeness and installation point and should be visible in the supplier comparison.
For turbidity sensor, the RFQ should make laboratory comparison and acceptance evidence visible before supplier comparison. If this Turbidity sensor requirement is omitted, a low initial quotation can later be offset by additional hardware, rewiring or repeat commissioning work.
The acceptance check should include process response after abnormal readings. This Turbidity sensor evidence confirms operation through the intended measurement, communication and response workflow rather than only a successful bench reading.
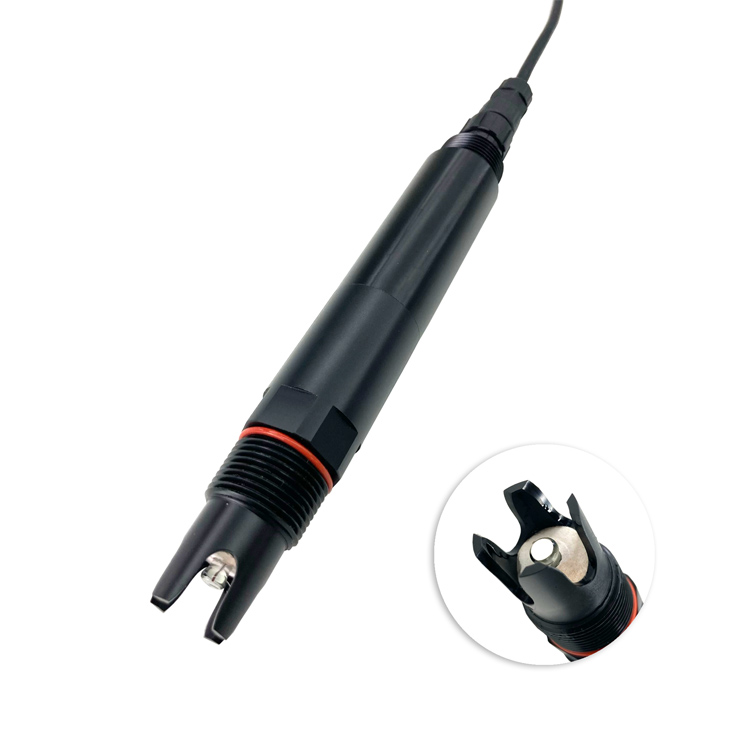
A1: For Turbidity sensor, confirm the expected range, water matrix, fouling risk, mounting method, power, protocol, cable length and the operating action linked to the reading. Without those details, the selected Turbidity sensor instrument may meet its bench specification yet fail to fit the process connection, controller or maintenance routine at site. During Turbidity sensor commissioning, verify this point and retain the result in the acceptance file.
A2: Specify online Turbidity sensor when continuous trends, remote alarms, PLC or RTU data exchange and unattended operation are project requirements. A handheld reference can verify Turbidity sensor during inspection, but it does not replace continuous logging where alarms, trends or remote operation are required. Define the responsible party and supporting evidence for Turbidity sensor before equipment approval.
A3: Install Turbidity sensor at a representative sample point, outside persistent bubbles and stagnant zones, with enough access for safe removal, cleaning and reference checks. Where Turbidity sensor is exposed to solids or biological growth, provide safe probe retrieval and set the cleaning method according to the observed fouling rate; a wiper or flow cell is justified only when the site needs it. Record this requirement in The turbidity sensor model-selection sheet before quotation.
A4: Use Turbidity sensor for continuous warning and process response while retaining laboratory analysis where the project requires compliance evidence or an independent reference. The operating procedure for Turbidity sensor should state when laboratory results are used for verification, investigation or compliance and how they are compared with the online trend. Selection of Turbidity sensor should begin with the measurement duty, site condition and receiving-system interface.
A5: The turbidity sensor handover file should contain the wiring definition, signal or register map, installation record, reference-check evidence, alarm settings and maintenance procedure applicable to the delivered configuration. During Turbidity sensor commissioning, verify this point and retain the result in the acceptance file.
A6: Specify Turbidity sensor as a complete package when the project also requires a controller, enclosure, gateway, power system, mounting assembly or several coordinated measurements at one point.
A7: Requesting the selected Turbidity sensor price before defining the site and integration scope produces quotations that are difficult to compare and often incomplete. The practical selection criteria for Turbidity sensor include the required measuring range, representative installation point and usable signal at the receiving controller. Record this requirement in The turbidity sensor model-selection sheet before quotation.
A8: An RFQ for Turbidity sensor should include the application, expected range, measured medium, mounting condition, output, cable length, quantity, destination and delivery schedule. The required class of Turbidity sensor depends on whether the project needs continuous data, remote alarms or documented handover records.
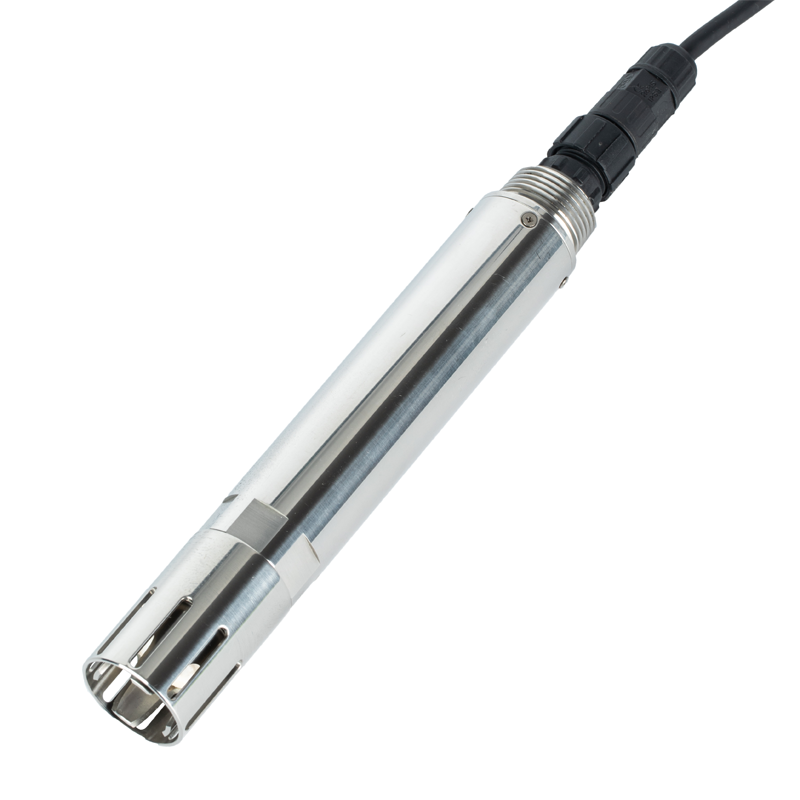
Turbidity sensor should help buyers turn an initial request into a project-ready specification. A complete Turbidity sensor review covers measurement range, output protocol, mounting, power, data handling, service access and acceptance evidence. With the installation environment and interface defined, NiuBoL can configure Turbidity sensor as a field device or as part of the required monitoring package.
Related recommendations
Sensors & Weather Stations Catalog
 Agriculture Sensors and Weather Stations Catalog-NiuBoL.pdf
Weather Stations Catalog-NiuBoL.pdf
Agriculture Sensors Catalog-NiuBoL.pdf
Water Quality Sensor Catalog-NiuBoL.pdf
Related products
 Combined air temperature and relative humidity sensor
 TDR Soil Moisture & Temperature Sensor for irrigation| RS485 |4-20mA| NBL-S-THR
 Soil pH sensor RS485 soil Testing instrument soil ph meter for agriculture |NBL-S-PH
 Wind Speed sensor Output Modbus/RS485/Analog/0-5V/4-20mA
 Tipping bucket rain gauge for weather monitoring auto rainfall sensor RS485/Outdoor/stainless steel
 Pyranometer Solar Radiation Sensor 4-20mA/RS485
Screenshot, WhatsApp to identify the QR code
WhatsApp number:+8615367865107
(Click on WhatsApp to copy and add friends)