





— Blogs —
—Products—
 Consumer hotline +8618073152920
WhatsApp:+8615367865107
Address:Room 102, District D, Houhu Industrial Park, Yuelu District, Changsha City, Hunan Province, China
Product knowledge
Time:2026-08-14 09:07:00 Popularity:270
Quick Answer: A water quality analyzer factory test should prove channel identity, measurement checks and the complete data path before shipment. It cannot establish that the eventual site sample is representative. Agree which checks use real probes and reference solutions, which use simulated inputs, and which must wait for site commissioning.
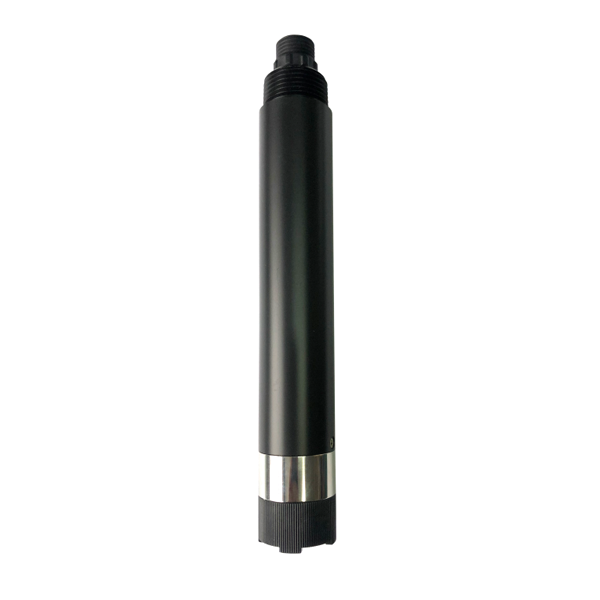
A water quality analyzer should be specified as a complete online analysis system, not as a single sensor name. In industrial and environmental monitoring projects, the analyzer may include probes, a controller or transmitter, cabinet wiring, power supply, communication, sampling structure, alarm settings and handover documents. The buyer should compare how the full system will operate after installation.
A water quality analyzer package can be simple or complex. Some projects need one probe and a transmitter. Others require a multi-parameter station with pH, conductivity, dissolved oxygen, turbidity, COD, ammonia nitrogen or other channels. The quotation should state what is included: probe, transmitter, bracket, cable, cabinet, logger, gateway, platform connection and documentation.
Use the ordered model list for the test, including range and output options. Record whether a gateway or destination platform is supplied or provided by the buyer. A substitute display used on the test bench cannot demonstrate a customer SCADA interface that was never connected.
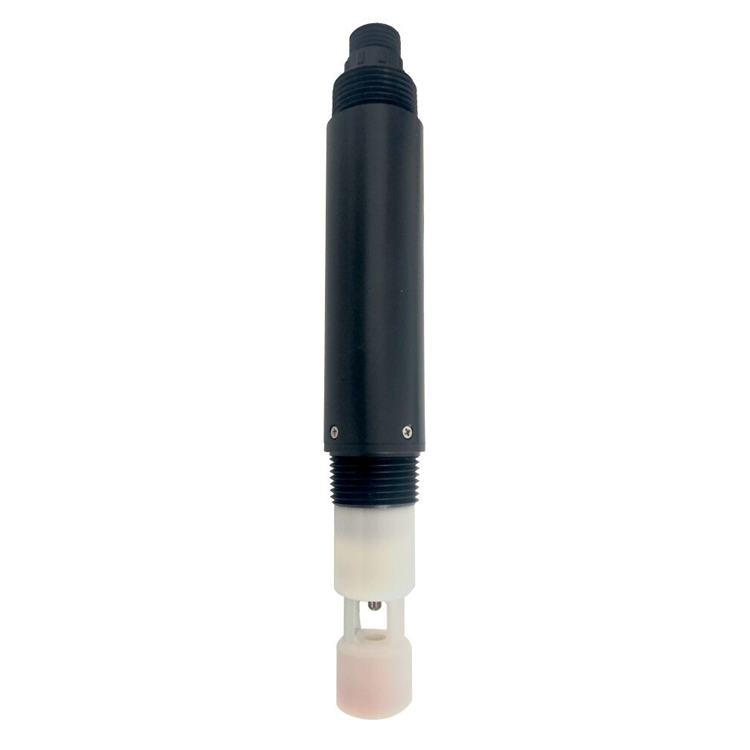
| Example instrument | Measurement basis and range | Factory test boundary |
|---|---|---|
| NBL-WQ-DO-4A | Optical DO; 0-20 mg/L; +/-2% of reading | Verify the reference procedure, temperature and configured compensation |
| NBL-WQ-EC-S | Electrode salinity; 0-70 PSU; +/-1.5% of reading | Verify unit and appropriate standard; do not relabel it as TDS |
| NBL-WQ-BOD-4S | Optical fluorescence; 0-300 mg/L | Separate instrument response checks from the site relationship to laboratory BOD5 |
| NBL-WQ-TS | 90-degree scattering turbidity; 20, 100 or 1000 NTU full-scale options | Test the ordered range using appropriate turbidity references |
| NBL-WQ-NHN | Ammonium ion-selective electrode; 10, 100 or 1000 mg/L full-scale options | Agree the reporting basis and reference method; consider the intended water matrix |
Specify an acceptance criterion for each ordered channel. A screen showing five values is not five independent reference checks. The optical BOD instrument below does not perform a five-day incubation simply because its output is labeled BOD; the process-water comparison remains a separate site task.
Record the reference, its preparation or certificate, sample temperature, stable instrument value and pass criterion. A simulated numerical input can test a screen or alarm, but it cannot establish probe accuracy or material compatibility.

Before production or shipment, confirm the cabinet wiring route, terminal allocation, grounding, surge protection and separation from pumps or dosing equipment. For RS485 Modbus RTU, each analyzer or probe should have documented address, baud rate, parity, register map, unit and decimal position.
The platform should display clear channel names, historical trends, alarm records and maintenance status. If the analyzer reports to a customer platform or SCADA system, the data mapping should be tested before site acceptance.
Follow a value from the labeled probe through the host to its intended record. Deliberately disconnect one channel in a safe test setup and check that only the corresponding point becomes unavailable. Restore it and verify recovery. Test alarm activation and reset through an agreed test method without treating a simulator result as a wet-probe measurement.
Power and immersion requirements are also model-specific. These five examples use 12-24 VDC, RS485 Modbus RTU, IP68 probe protection and standard 5 m cables; confirm delivered cable jackets and options. DO-4A, EC-S, BOD-4S and TS list 0.2 W at 12 V, as does NHN. The cabinet, gateway and sample equipment require a separate complete-system power budget.
It can establish that the specified equipment is assembled and that agreed measurement, communication and software tests pass in the recorded conditions. It does not demonstrate representative sampling at a site that has not yet been commissioned.
No. Simulation is useful for labels, scaling, alarms and fault logic. A real-probe check is needed to evaluate instrument response, using a suitable reference and model-specific procedure.
Yes. Confirm the physical probe, register map, units and reference result for each channel. One successful Modbus response or one calibrated probe does not validate the rest of the analyzer.
Request the tested model/range list, results against agreed criteria, wiring and data maps, saved configuration and unresolved items. Clearly mark tests that still depend on the customer's site or platform.
Check sample representativeness, pressure, temperature, flow or immersion, fouling and safe maintenance access. Complete process-water comparisons and operational alarm tests under the installation's actual conditions.
No. A bench response confirms the tested instrument behavior. The relationship between an optical estimate and the required laboratory method must be assessed using representative site water and agreed acceptance criteria.
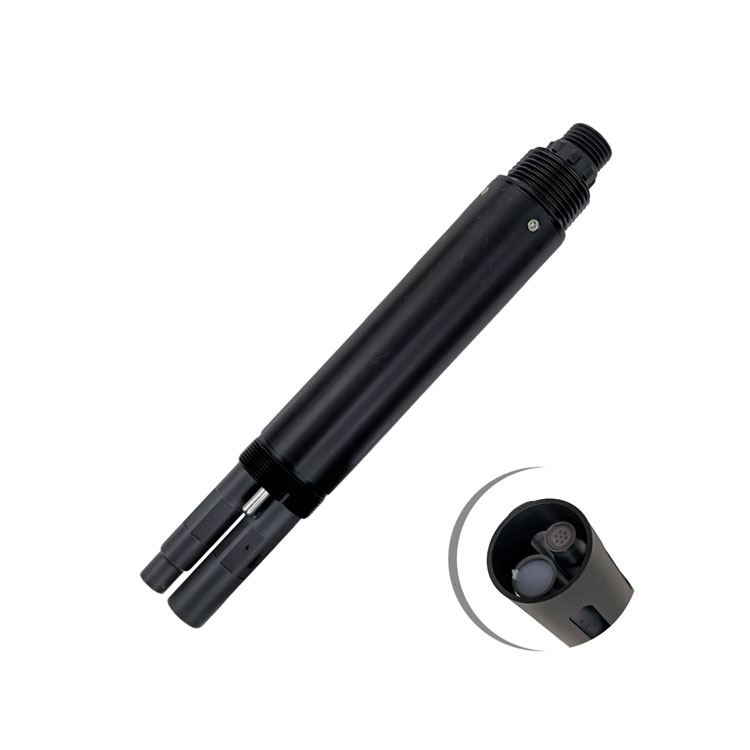
A water quality analyzer factory test is useful when every result is tied to a defined instrument, reference and destination record. Complete assembly and interface tests before shipment, distinguish simulation from measurement, and identify the site checks still required for commissioning. Send NiuBoL the channel list and acceptance requirements when requesting an analyzer configuration.
Prev:Weather Underground Station Integration: Verify the Gateway Before Ordering
Next:Rain Gauge Price for Bulk Projects: Pilot Approval and Repeat-Order Checks
Related recommendations
Sensors & Weather Stations Catalog
 Agriculture Sensors and Weather Stations Catalog-NiuBoL.pdf
Weather Stations Catalog-NiuBoL.pdf
Agriculture Sensors Catalog-NiuBoL.pdf
Water Quality Sensor Catalog-NiuBoL.pdf
Related products
 Combined air temperature and relative humidity sensor
 TDR Soil Moisture & Temperature Sensor for irrigation| RS485 |4-20mA| NBL-S-THR
 Soil pH sensor RS485 soil Testing instrument soil ph meter for agriculture |NBL-S-PH
 Wind Speed sensor Output Modbus/RS485/Analog/0-5V/4-20mA
 Tipping bucket rain gauge for weather monitoring auto rainfall sensor RS485/Outdoor/stainless steel
 Pyranometer Solar Radiation Sensor 4-20mA/RS485


Screenshot, WhatsApp to identify the QR code
WhatsApp number:+8615367865107
(Click on WhatsApp to copy and add friends)

