
— Blogs —
—Products—
 Consumer hotline +8618073152920
WhatsApp:+8615367865107
Address:Room 102, District D, Houhu Industrial Park, Yuelu District, Changsha City, Hunan Province, China
Product knowledge
Time:2026-08-22 09:05:00 Popularity:152
Reliable measurement with Systronics Turbidity Meter depends as much on bubble control, fouling management and representative flow as on the analyzer specification. The engineering test for Systronics Turbidity Meter is its ability to withstand the installation environment, exchange data with the controller and maintain readings that remain credible after handover.
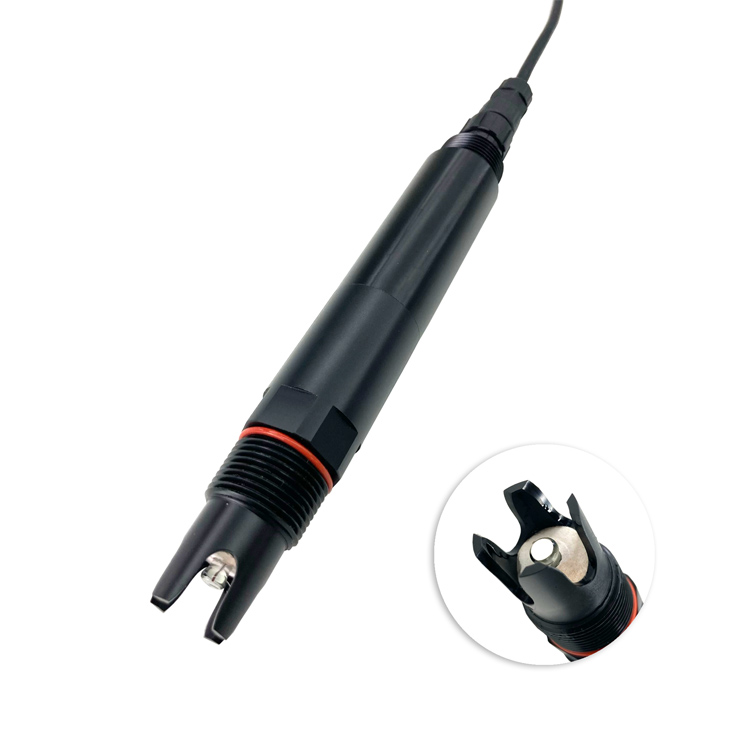
The term systronics turbidity meter often hides several different needs: spot checking, continuous monitoring, automation control, remote data upload or quotation comparison.
For systronics turbidity meter, the buyer should write the use case in one sentence before comparing suppliers. For systronics turbidity meter, the use case should identify whether the measurement supports process control, an alarm, an operating schedule, a reference record or an environmental warning. Defining that duty for Systronics Turbidity Meter determines the range, interface, accessories and evidence required at handover.
Buyers normally search systronics turbidity meter after seeing a field problem: unstable readings, manual sampling cost, unclear supplier quotes or an installation that cannot connect to the existing system. The result should be the selected Systronics Turbidity Meter specification that installers, control engineers and procurement teams can evaluate against the same operating requirement.
Searches around systronics turbidity meter often come from users familiar with consumer or DIY equipment. That equipment can be useful for learning or simple spot checks. For engineering projects, the stronger requirement is documented output, stable power, serviceable installation and a supplier who can support wiring, register maps and project quantities.
The practical acceptance test for systronics turbidity meter is not only powering on the device. Handover for Systronics Turbidity Meter should demonstrate a valid live reading, successful controller communication, the intended alarm path and one routine service procedure performed by site staff.
For systronics turbidity meter, remote station power and telemetry reliability should be written into the purchase file. For Systronics Turbidity Meter, a comparable quotation should separate the sensing assembly, signal interface, cable, mounting accessories and commissioning services required by the stated site conditions.
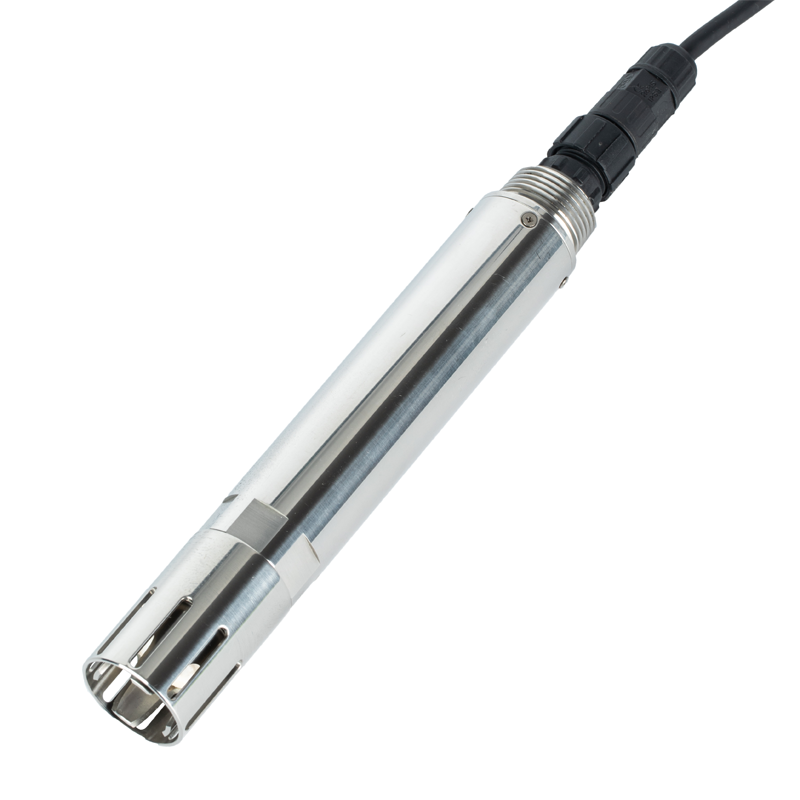
For systronics turbidity meter, Modbus communication should be checked against the actual water quality cabinet: register address, unit, decimal place, temperature compensation value and alarm polling interval all need to be confirmed before shipment.
For systronics turbidity meter, the cable route should be checked against pumps, dosing lines and aeration equipment. The turbidity meter cable route, shield termination, grounding arrangement and junction-box location should be verified with the control-panel design before installation.
For turbidity meter, process response after abnormal readings should be written into the purchase file. For Turbidity meter, a comparable quotation should separate the sensing assembly, signal interface, cable, mounting accessories and commissioning services required by the stated site conditions.
| Parameter | Typical project value | Procurement meaning |
|---|---|---|
| Measurement range for turbidity meter | Selected by parameter and water matrix | Prevents low resolution or overload at the alarm point |
| Accuracy for turbidity meter | Project-grade online accuracy after calibration | Supports trend alarms and process control |
| Power supply for turbidity meter | DC 12-24 V | Fits water quality cabinets and solar monitoring points |
| Output for turbidity meter | RS485 Modbus RTU | Allows direct connection to PLC, RTU, data logger or IoT gateway |
| Protection for turbidity meter | IP68 probe or flow-through assembly | Matches immersion, tank, channel or pipeline installation |
| Maintenance for turbidity meter | Cleaning and calibration interval by fouling level | Often decides long-term data reliability |
Field challenge: A turbidity meter may be used as an existing plant or laboratory reference, but its measurement method, sample handling and output must be identified before it is compared with an online immersion probe. A brand name alone does not establish equivalent range, response or integration scope.
Integration plan for Turbidity meter: Install online sensors with RS485 output and safe retrieval for cleaning.
Project value: continuous Turbidity meter data provides earlier warning of unstable water conditions and gives operators a record for evaluating corrective action.
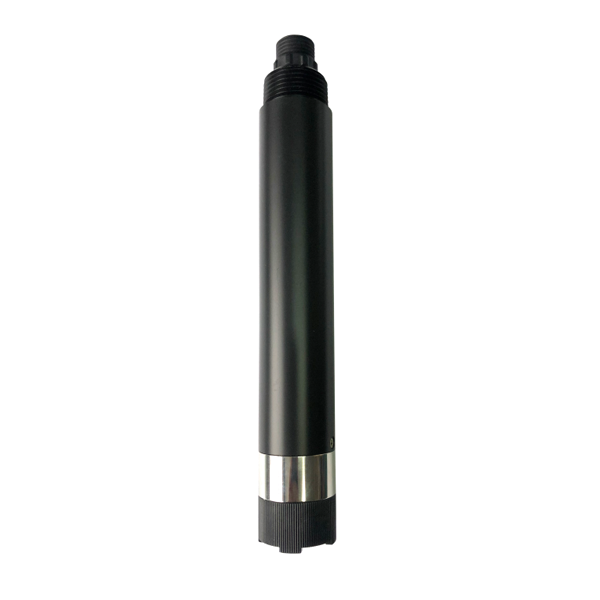
Field challenge: For Turbidity meter, wastewater grease, suspended solids, bubbles and deposits must be considered when choosing the mounting point and cleaning interval.
Integration plan for Turbidity meter: select a serviceable probe position, provide secure mounting and leave enough access for inspection, cleaning and reference checks without interrupting the process unnecessarily.
Project value: online Turbidity meter trends show changes between laboratory sampling rounds and support a faster, documented operating response.
Field challenge: At a river or source-water site, Turbidity meter must remain representative as water level, debris load and biological growth change through the season.
Integration plan for A turbidity meter: document whether readings come from a bench sample, flow-through cell or installed probe, then define sample collection, settling limits, cleaning, comparison frequency and any manual or digital transfer to the plant record. Do not map laboratory values to a control loop without time and sample-point context.
Project value: reliable Turbidity meter trends help operators distinguish a developing water-quality change from a short communication or maintenance event.
For Turbidity meter, commissioning should record power voltage, output signal, live data, alarm threshold, cable labels and installation position. Retain The turbidity meter test record with the handover documents so later maintenance can distinguish configuration changes from sensor or process changes.
For long-term operation, turbidity meter should be purchased with a spare-parts view. For Turbidity meter, cable assemblies, mounting parts and service consumables should be reviewed as availability-critical items because a missing minor component can stop a monitoring point.
If the project includes several monitoring points, create a small point list for turbidity meter: ID, location, cable length, Modbus address, parameter unit and maintenance note. The turbidity meter point schedule becomes the common reference for address assignment, commissioning records, maintenance history and later system expansion.
For turbidity meter, the specification should name the operating decision first. Where Turbidity meter data initiates an alarm, the specification should identify the threshold, delay logic, responsible operator and required response rather than relying on a feature list. Where Turbidity meter supports reporting rather than control, stable sampling intervals, timestamps, engineering units and export format become the principal data requirements.
A supplier comparison for turbidity meter should separate the sensor, accessories, controller interface, mounting hardware, documentation and after-sales support. Separating these scope items allows Turbidity meter offers to be compared on equivalent hardware, integration and service responsibilities.
Before requesting a quotation for turbidity meter, provide the application site, expected measuring range, installation method, power supply, required output, cable length, quantity, destination country, accessories and whether local display or remote platform upload is required.
For turbidity meter, maintenance cost and spare probe planning should be written into the purchase file. For Turbidity meter, a comparable quotation should separate the sensing assembly, signal interface, cable, mounting accessories and commissioning services required by the stated site conditions.
The project should evaluate turbidity meter mainly from the angle of controller integration and Modbus register mapping. For Turbidity meter, that operating focus changes the required evidence for controller integration and Modbus register mapping and should be visible in the supplier comparison.
For turbidity meter, the RFQ should make remote station power and telemetry reliability visible before supplier comparison. If this Turbidity meter requirement is omitted, a low initial quotation can later be offset by additional hardware, rewiring or repeat commissioning work.
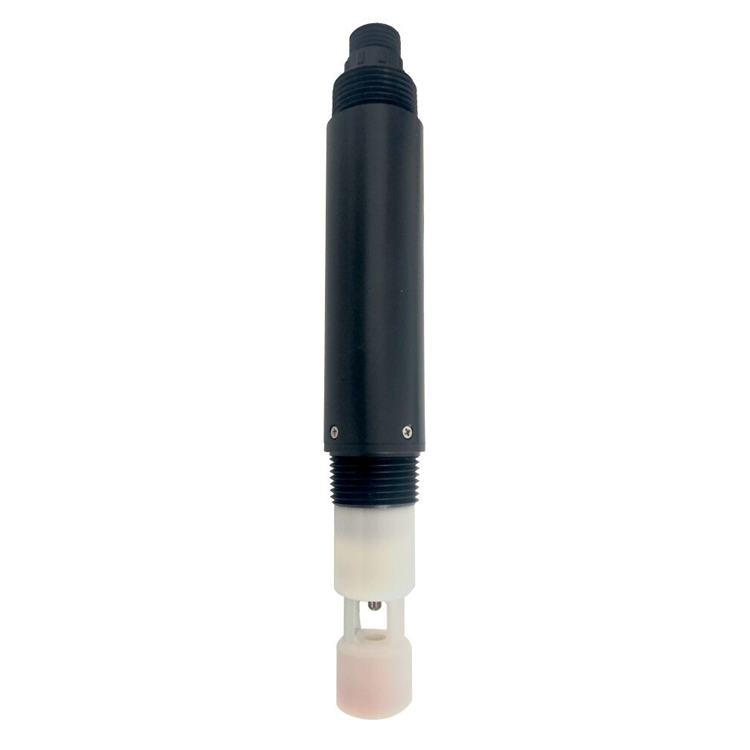
A1: For Turbidity meter, confirm the expected range, water matrix, fouling risk, mounting method, power, protocol, cable length and the operating action linked to the reading. Without those details, the selected Turbidity meter instrument may meet its bench specification yet fail to fit the process connection, controller or maintenance routine at site. For Turbidity meter Industrial Online Water Quality Sensor, record this requirement in the model-selection sheet before quotation.
A2: Specify online Turbidity meter when continuous trends, remote alarms, PLC or RTU data exchange and unattended operation are project requirements. A handheld reference can verify Turbidity meter during inspection, but it does not replace continuous logging where alarms, trends or remote operation are required. Selection of Turbidity meter should begin with the measurement duty, site condition and receiving-system interface.
A3: Install Turbidity meter at a representative sample point, outside persistent bubbles and stagnant zones, with enough access for safe removal, cleaning and reference checks. Where Turbidity meter is exposed to solids or biological growth, provide safe probe retrieval and set the cleaning method according to the observed fouling rate; a wiper or flow cell is justified only when the site needs it. During Turbidity meter commissioning, verify this point and retain the result in the acceptance file.
A4: Use Turbidity meter for continuous warning and process response while retaining laboratory analysis where the project requires compliance evidence or an independent reference. The operating procedure for Turbidity meter should state when laboratory results are used for verification, investigation or compliance and how they are compared with the online trend. For Turbidity meter Industrial Online Water Quality Sensor, define the responsible party and supporting evidence before equipment approval.
A5: The turbidity meter handover file should contain the wiring definition, signal or register map, installation record, reference-check evidence, alarm settings and maintenance procedure applicable to the delivered configuration.
A6: Specify Turbidity meter as a complete package when the project also requires a controller, enclosure, gateway, power system, mounting assembly or several coordinated measurements at one point. The required class of Turbidity meter depends on whether the project needs continuous data, remote alarms or documented handover records.
A7: Requesting the selected Turbidity meter price before defining the site and integration scope produces quotations that are difficult to compare and often incomplete. The practical selection criteria for Turbidity meter include the required measuring range, representative installation point and usable signal at the receiving controller. During Turbidity meter commissioning, verify this point and retain the result in the acceptance file.
A8: For a replacement or comparison enquiry, provide the existing Systronics model, measurement method, range, sample arrangement, output, accessories, observed fault and required role of the new instrument. Include the target water, controller or reporting method, quantity and delivery destination so functional equivalence can be assessed.

Turbidity meter should help buyers turn an initial request into a project-ready specification. A complete Turbidity meter review covers measurement range, output protocol, mounting, power, data handling, service access and acceptance evidence. With the installation environment and interface defined, NiuBoL can configure Turbidity meter as a field device or as part of the required monitoring package.
For turbidity meter, controller integration and Modbus register mapping should be written into the purchase file. For Turbidity meter, a comparable quotation should separate the sensing assembly, signal interface, cable, mounting accessories and commissioning services required by the stated site conditions.
Prev:Dirt Humidity Sensor: Project Selection Guide for Weather and Environmental Monitoring
Next:Instrument to Measure TDS in Water: Industrial Selection Guide for Online Monitoring Projects
Related recommendations
Sensors & Weather Stations Catalog
 Agriculture Sensors and Weather Stations Catalog-NiuBoL.pdf
Weather Stations Catalog-NiuBoL.pdf
Agriculture Sensors Catalog-NiuBoL.pdf
Water Quality Sensor Catalog-NiuBoL.pdf
Related products
 Combined air temperature and relative humidity sensor
 TDR Soil Moisture & Temperature Sensor for irrigation| RS485 |4-20mA| NBL-S-THR
 Soil pH sensor RS485 soil Testing instrument soil ph meter for agriculture |NBL-S-PH
 Wind Speed sensor Output Modbus/RS485/Analog/0-5V/4-20mA
 Tipping bucket rain gauge for weather monitoring auto rainfall sensor RS485/Outdoor/stainless steel
 Pyranometer Solar Radiation Sensor 4-20mA/RS485
Screenshot, WhatsApp to identify the QR code
WhatsApp number:+8615367865107
(Click on WhatsApp to copy and add friends)