





— Blogs —
—Products—
 Consumer hotline +8618073152920
WhatsApp:+8615367865107
Address:Room 102, District D, Houhu Industrial Park, Yuelu District, Changsha City, Hunan Province, China
Product knowledge
Time:2026-08-08 13:42:22 Popularity:349
Quick Answer: An industrial turbidity sensor is suitable only when its wetted materials, optical window, temperature and pressure limits match the actual process water. IP68 does not establish resistance to hot cleaning chemicals, abrasive slurry or every corrosive liquid. If direct immersion exceeds a limit, evaluate a representative conditioned sample or another instrument instead of relying on a stronger-looking housing.
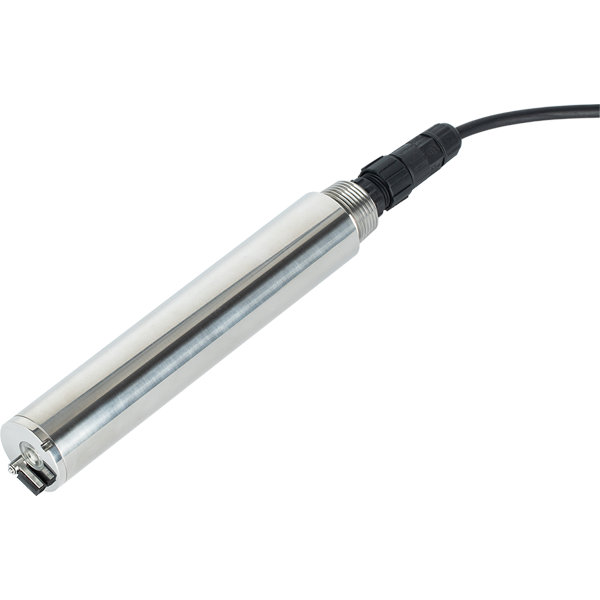
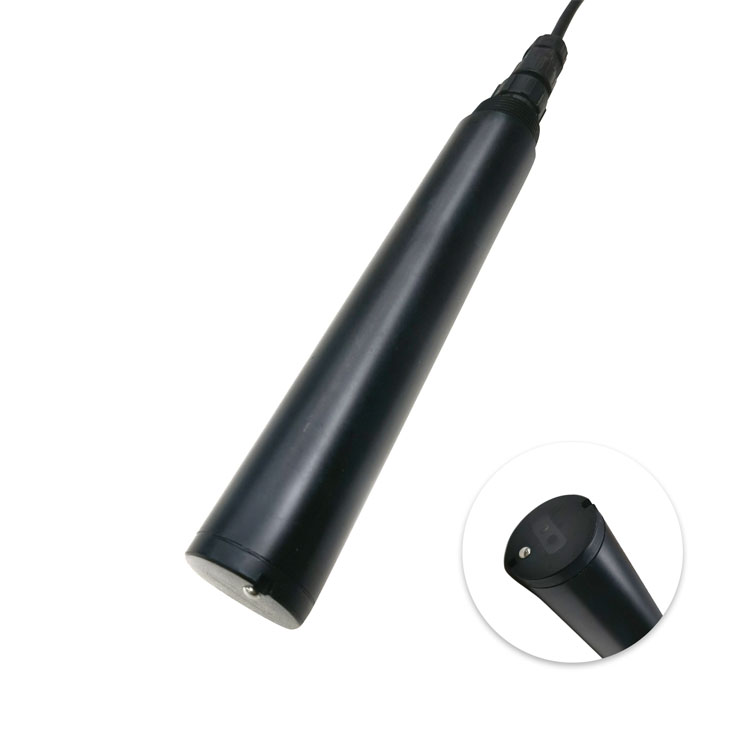
The NiuBoL TS-408-S uses a 316L stainless steel housing and quartz optical components. Those materials are relevant to selection, but they are not a blanket approval for concentrated acids, oxidizing cleaners or abrasive particles. The seals, cable entry, connector and any cleaning mechanism also contact or encounter the process environment.
Send the liquid composition and cleaning sequence with the inquiry. Include concentration, temperature, exposure duration and whether cleaning occurs while the instrument remains installed. A probe may tolerate normal production water but not the hotter or more concentrated cleaning stage. Material selection has to cover both, or the installation must provide a safe way to isolate and remove the instrument.
For hot or pressurized water, a cooled and pressure-controlled sample may protect an instrument that cannot enter the main process. However, the resulting turbidity must still represent the water of interest. Long lines can retain deposits, allow particles to settle or delay a short contamination event. Pressure reduction can also release bubbles that affect optical readings.
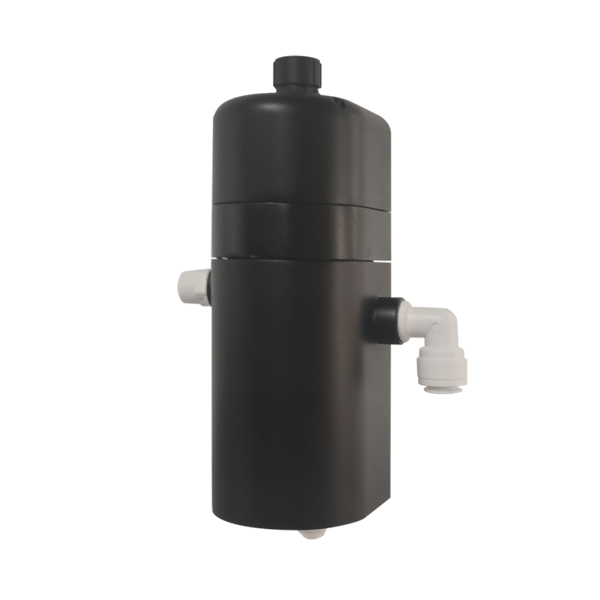
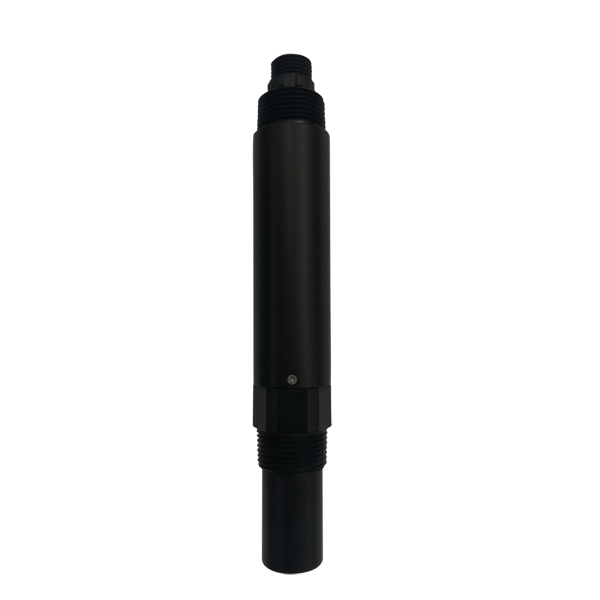
The TSA-4 flow-through instrument is intended for low-range monitoring, not for receiving an unrestricted industrial bypass. It needs controlled sample conditions and a drain arrangement. Its IP65 enclosure must remain outside the water; a flow cell is not an immersion-rated probe.
| Instrument | Relevant specifications | Limit on the selection decision |
|---|---|---|
| TS-408-S immersion turbidity probe | 316L and quartz; IP68; configured 0-100, 0-1000 or 0-4000 NTU; RS485 Modbus RTU; optional 4-20 mA | Obtain the configuration-specific chemical, pressure and temperature limits; do not infer abrasion resistance from the housing material |
| TSA-4 flow-through instrument | 0-10 NTU; 0-50 C; pressure no higher than 0.2 MPa; inlet flow no higher than 300 mL/min; composite housing; IP65 | Requires controlled sampling and wall mounting; unsuitable as a submerged slurry probe |
| Base NBL-WQ-TS | Configured 0-20, 0-100 or 0-1000 NTU; 0-50 C; pressure below 0.2 MPa; POM/ABS housing; IP68 | Its construction and range options differ from the TS-408-S; assess the actual supplied variant |
For the base NBL-WQ-TS, the supply is 12-24 VDC, consumption is 0.2 W at 12 V and standard cable length is 5 m. Those figures do not define a complete sampling station's power demand. Ask separately about the cable jacket and seals when solvents, outdoor exposure or repeated cleaning are involved.
A configurable multiparameter assembly can place turbidity beside pH, conductivity or dissolved oxygen at one monitoring point. It is useful when the channels belong in the same water. It does not make that location acceptable for every fitted module. The lowest applicable temperature, pressure or chemical limit may govern the arrangement.
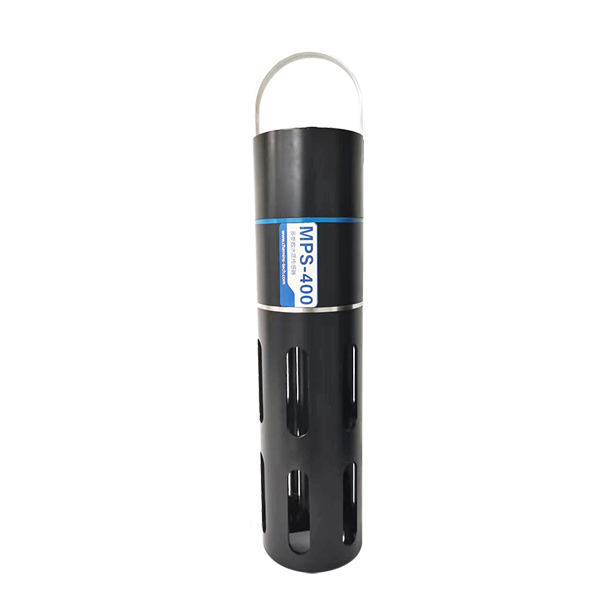
In a neutralization process, for example, the pH channel and turbidity channel may need different locations or service intervals. Check whether local dosing creates a concentrated plume before the water is mixed. A shared head placed in that plume can expose several modules to a condition that is not representative of the bulk water.
An industrial turbidity sensor measures an optical response, not the identity or mass of every suspended material. Particle size, particle color, liquid color, bubbles and deposits can change the result. A high NTU range does not establish a validated TSS output in mg/L. Where solids concentration is the decision variable, evaluate a dedicated measurement or a site-specific correlation against suitable laboratory results.
Before approving the location, compare normal production, startup, cleaning and upset conditions. Observe whether spikes follow pump starts, air entrainment or a cleaning cycle. Keep these observations separate from calibration: changing calibration to suppress a bubble-induced spike can damage the validity of otherwise useful readings.
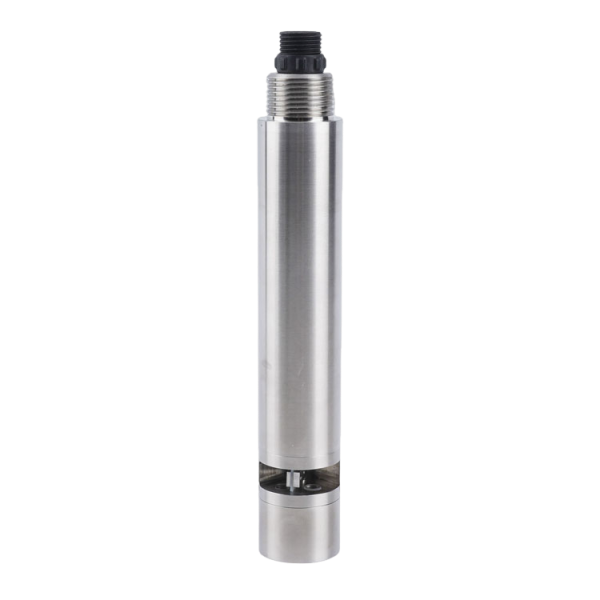
An optical COD probe belongs to a different measurement task. It may help investigate organic loading alongside turbidity, but a COD value cannot confirm that a turbidity channel is correct. Nor does a turbidity peak establish an equivalent COD increase. If both channels are required, identify the water question and applicable range for each before combining them in a monitoring station.
For an abrasive stream, assess particle size, solids loading, velocity and the chance of impact on the optical end. Avoid positioning a probe in a direct solids jet. The TS-408-S installation guidance calls for at least 5 cm clearance from side walls and 10 cm from the bottom. Allow additional service space for safe removal without pulling the cable.
Test a representative installation through a normal operating and cleaning sequence. Inspect the window, housing, cable and seals afterward, and compare checks before and after cleaning. A short trial can reveal immediate incompatibility; it cannot prove unlimited service life. If the site cannot provide safe access, revise the mounting or sampling arrangement before purchase.
Read the selected model on the intended PLC, RTU or data logger using its own RS485 Modbus RTU register map. Keep cleaning and maintenance states out of normal process evaluation where the controller supports that distinction. Communication success alone does not establish that the sample is representative or the wetted materials are suitable.
No. Ingress protection and chemical compatibility are separate requirements. Evaluate the complete wetted construction against composition, concentration, temperature and cleaning exposure. A housing rating does not establish resistance to a particular liquid.
Only if the full exposure stays within the ordered instrument's limits. Otherwise provide approved isolation and removal or a suitable conditioned sample arrangement. Normal-water temperature alone is insufficient for this decision.
No. Suitability depends on the chemical and mechanical duty. A selected polymer may suit one liquid while stainless steel suits another. Compare all wetted components and the cleaning procedure rather than ranking housings by appearance.
A turbidity range does not establish a solids mass-concentration calibration. Test the actual slurry for optical suitability and, where required, establish a separate validated relationship to TSS. Check abrasion and fouling risks independently.
Provide water and cleaning chemistry, normal and upset temperature and pressure, particle loading, expected NTU range, mounting sketch and controller interface. Include photographs showing access and the proposed optical clearance. NiuBoL can then assess a specific configuration rather than an undefined harsh-environment requirement.
Select an industrial turbidity sensor by the complete exposure and measurement duty, not IP rating alone. Decide whether direct immersion or controlled sampling preserves both instrument suitability and representative data. Share the process and cleaning conditions with NiuBoL before specifying the probe, fittings and receiving interface.
Prev:Automatic Irrigation System Using Arduino: RS485 Soil Sensor and Valve Control
Next:Turbidity Meters for Online Monitoring: Retrofit a 4-20 mA Input
Related recommendations
Sensors & Weather Stations Catalog
 Agriculture Sensors and Weather Stations Catalog-NiuBoL.pdf
Weather Stations Catalog-NiuBoL.pdf
Agriculture Sensors Catalog-NiuBoL.pdf
Water Quality Sensor Catalog-NiuBoL.pdf
Related products
 Combined air temperature and relative humidity sensor
 TDR Soil Moisture & Temperature Sensor for irrigation| RS485 |4-20mA| NBL-S-THR
 Soil pH sensor RS485 soil Testing instrument soil ph meter for agriculture |NBL-S-PH
 Wind Speed sensor Output Modbus/RS485/Analog/0-5V/4-20mA
 Tipping bucket rain gauge for weather monitoring auto rainfall sensor RS485/Outdoor/stainless steel
 Pyranometer Solar Radiation Sensor 4-20mA/RS485


Screenshot, WhatsApp to identify the QR code
WhatsApp number:+8615367865107
(Click on WhatsApp to copy and add friends)

